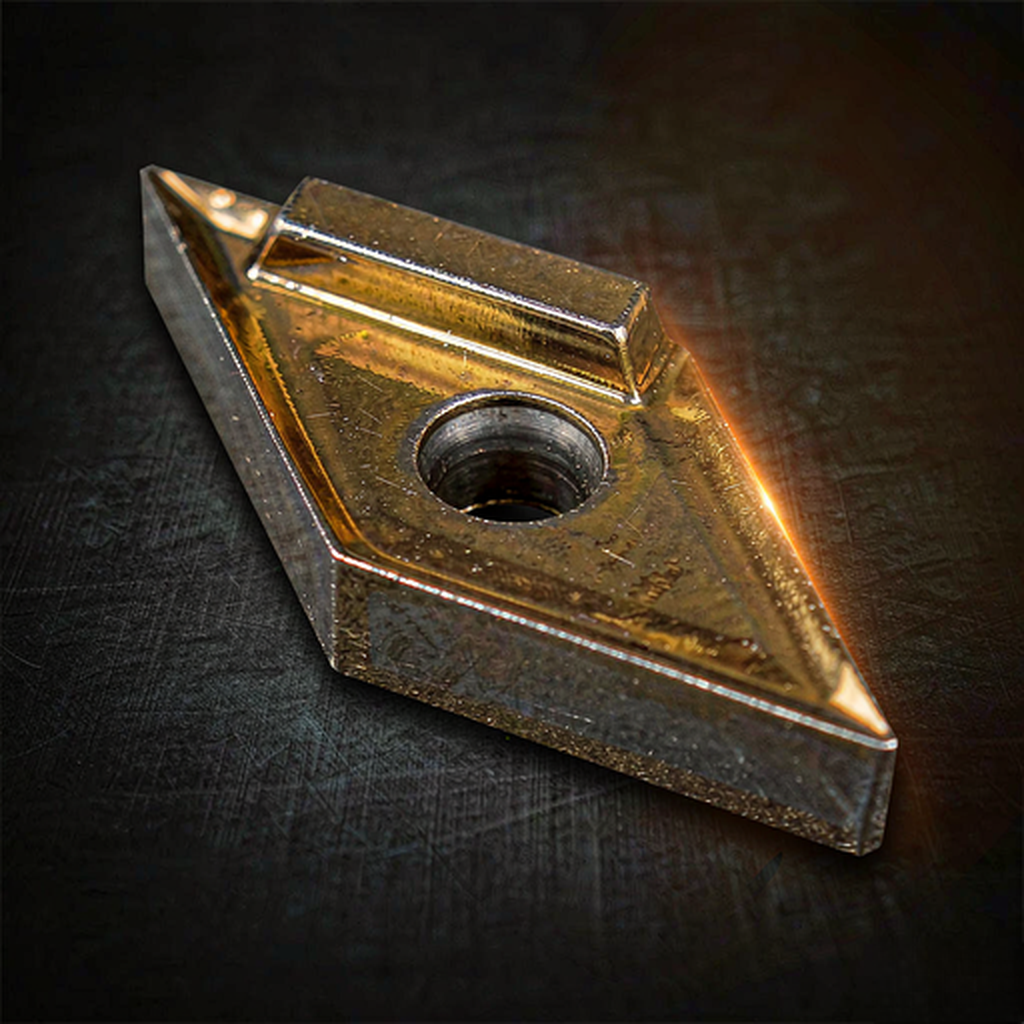
Milling Inserts · APMT Series
DM-APMT1135PDER-M2
General-purpose indexable milling insert with molded chipbreaker. First choice for shoulder milling and face milling in steel and stainless steel.
Workpiece materials:
PMK
- ISO designationAPMT 1135 PDER
- Cutting edge length11 mm
- Thickness3.5 mm
- Corner radius0.8 mm
- ChipbreakerM2 (medium)
- MOQ10 pcs
Available Grades
| Grade | Coating | ISO Range | Recommended For | Feature |
|---|---|---|---|---|
| DM5130 | PVD TiAlN | P15–P35 | Carbon & alloy steel, general milling | Sharp edge, low cutting force |
| DM5135 | PVD AlTiN | M20–M40 | Stainless steel, HRSA finishing | Heat-resistant, anti-built-up edge |
| DM3225 | CVD TiCN+Al₂O₃ | K10–K30 | Cast iron, high-speed dry cutting | Thick coating, wear resistant |
Dimension Table (APMT Series)
| Model | L (mm) | S (mm) | r (mm) | d (mm) | Available Grades |
|---|---|---|---|---|---|
| DM-APMT1135PDER-M2 | 11.0 | 3.5 | 0.8 | 6.35 | DM5130 / DM5135 / DM3225 |
| DM-APMT1135PDER-H2 | 11.0 | 3.5 | 0.8 | 6.35 | DM5135 / DM3225 |
| DM-APMT1604PDER-M2 | 16.5 | 4.76 | 0.8 | 9.525 | DM5130 / DM5135 / DM3225 |
| DM-APMT1604PDER-H2 | 16.5 | 4.76 | 0.8 | 9.525 | DM5135 / DM3225 |
Recommended Cutting Data
| Material | Hardness | Vc (m/min) | fz (mm/tooth) | ap (mm) |
|---|---|---|---|---|
| P Carbon steel | HB180–280 | 150–260 | 0.08–0.20 | ≤ 4.0 |
| M Stainless steel | HB180–250 | 120–200 | 0.06–0.15 | ≤ 3.0 |
| K Cast iron | HB150–260 | 160–300 | 0.10–0.25 | ≤ 5.0 |
* Values are starting recommendations for DM5130 grade with coolant. Adjust per machine rigidity and setup.
Technical Drawing
2D drawing (PDF / DXF) available on request — mention the model number in your inquiry.
Compatible Cutter Bodies
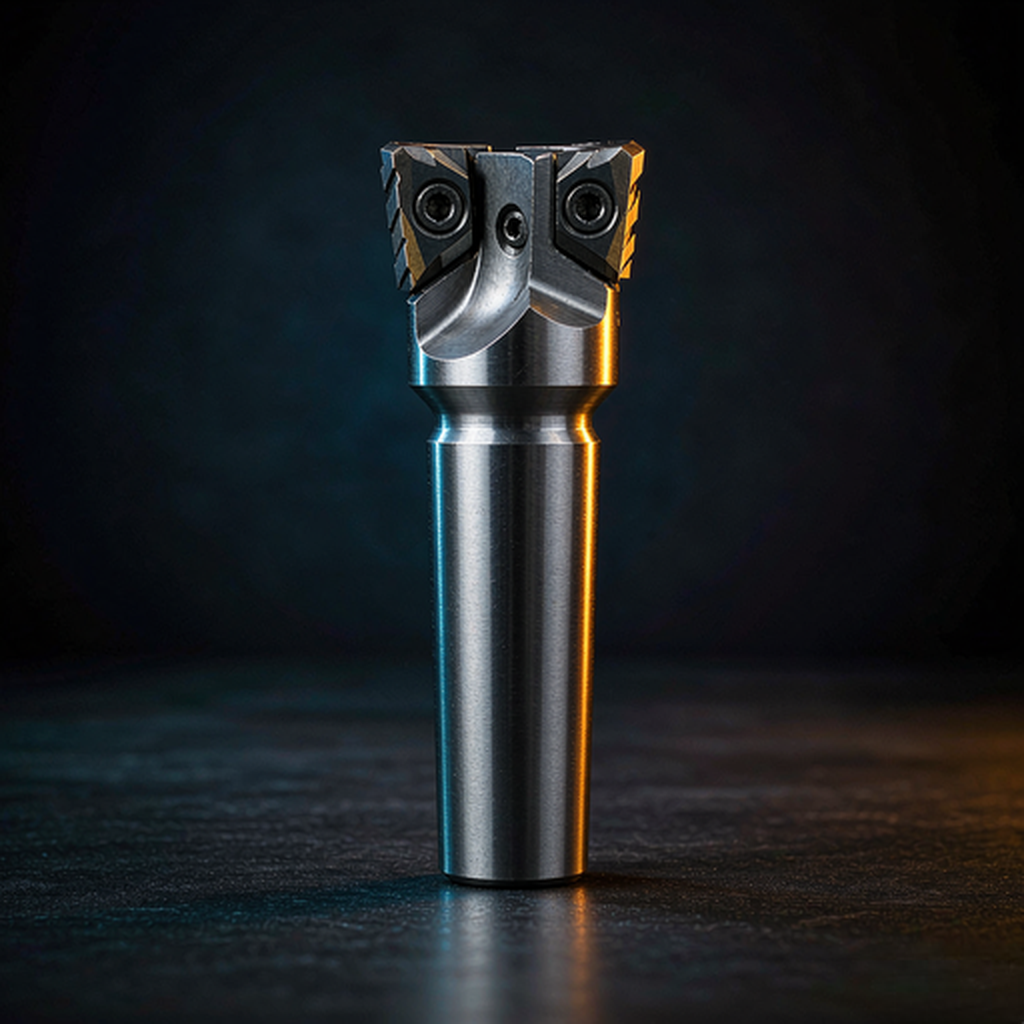
DM90-032B32-AP11
90° Shoulder Mill Ø32
DM90-040B32-AP11
90° Shoulder Mill Ø40
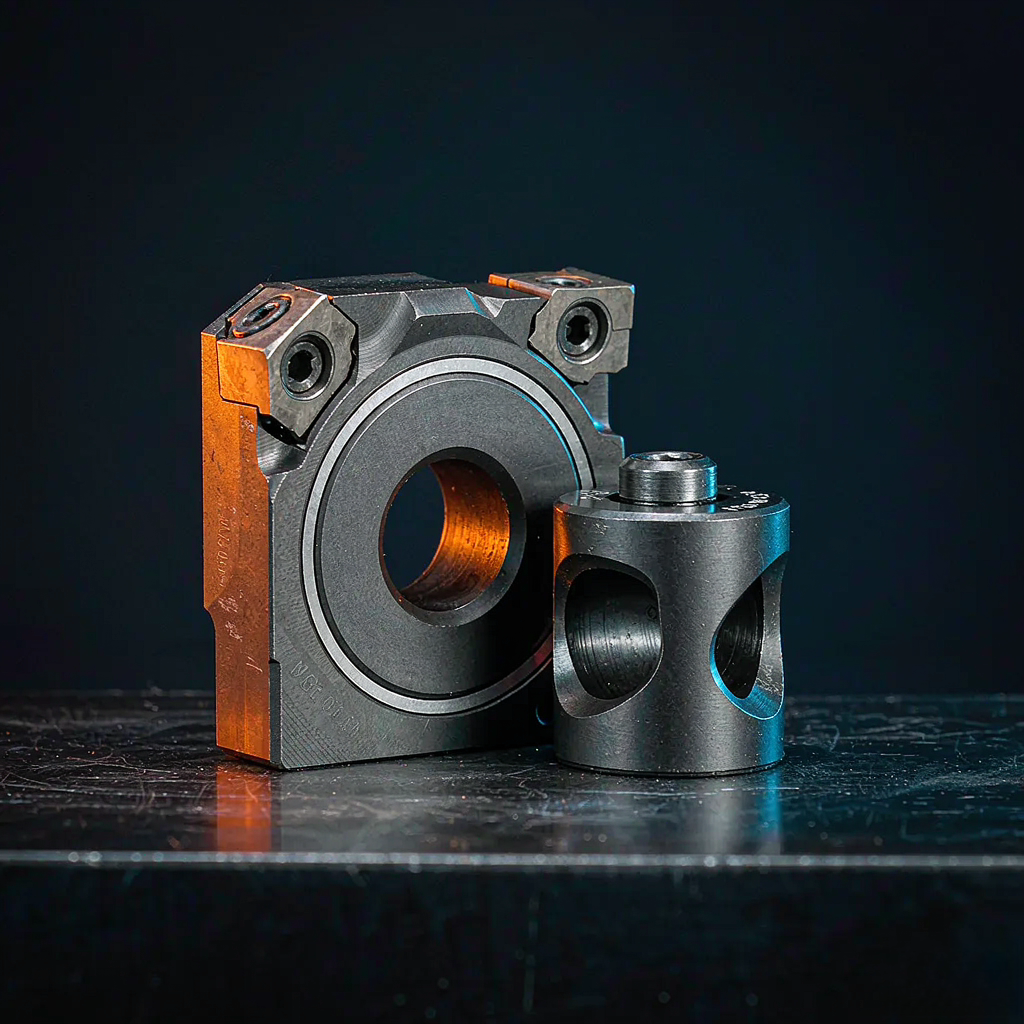
DM90-063A22-AP11
90° Face Mill Ø63
ⓘNeed a different corner radius or chipbreaker? Custom Tooling →